저희는 중국에 본사를 둔 선도적인 유리 제조업체로,
산업 및 건축 분야를 위한 고품질 유리 솔루션을 전문으로 합니다.
다년간의 경험과 ISO 인증을 바탕으로, 전 세계의 조달 전문가, 엔지니어 및 프로젝트 관리자에게 신속하고 맞춤형 견적과 신속한 지원을 제공합니다.
Low-E Edge Deletion is often treated as a routine fabrication action. That is precisely why it should have more detailed examination.
A clean-looking side does not always show full covering removal, right removal width, or compatibility with the shielding glass system (IGU) sealer system. Residual coating, contamination, and excessive abrasion can stay unseen till the system is constructed or weakens in solution.
Look is not acceptance. Makers need recorded process controls, quantifiable requirements, and traceable assessment documents– not just an operator’s judgment that the side looks clean.
The goal is to remove the defined layer regularly without damaging the glass or compromising the designated edge-seal design.
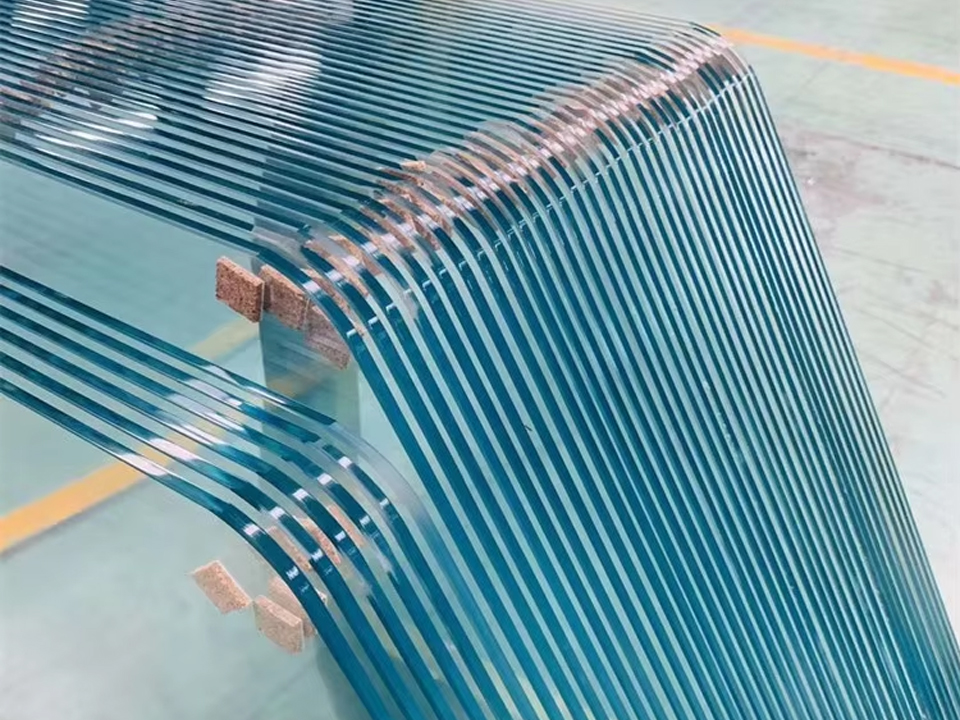
Low-E layers reduce radiative warm transfer and enhance glazing power efficiency. Lots of sputtered soft-coat items consist of silver-based useful layers that can be vulnerable to deterioration when subjected to wetness or inappropriate chemicals.
Side deletion gets rid of the specified covering from the perimeter where the approved IGU securing system needs it. This helps develop the designated bonding surface and lowers the risk of coating-related wear and tear.
Three concerns should lead assessment:
A pane can pass one check and stop working an additional. That is why visual evaluation alone wants.
In its June 2024 technical publication, Cardinal IG’s assistance on side removal of sputtered LoĒ finishes discusses that eliminating the layer layers supports sealant bonding to glass and helps in reducing the possibility for corrosion, delamination, and compromised seal honesty. These instructions put on the specified Cardinal products; various other finishings require their own accepted manufacture support.
Prior to processing, confirm the coating product, pane orientation, removal demands, and designated edge-seal configuration.
The production documentation must determine:
Do not presume that two visually similar coatings have identical handling requirements. Product replacements ought to set off a technological review when their fabrication instructions vary.
Mechanical grinding or abrasion is generally utilized for finish elimination. Relevant variables consist of wheel problem, removal-head position, used pressure, feed rate, glass placement, and path consistency.
There is no global machine establishing that suits every coating and production line. Develop an authorized operating home window based on tools capability, layer directions, and verified results.
A worn abrasive can leave residual finish also when small settings have actually not changed. Enhancing pressure without recognizing the reason may instead broaden the deletion band or damages the glass.
Tape-record significant operating criteria and validate the arrangement after upkeep, tooling replacement, or program changes.
The needed deletion zone ought to be continuous along every specified edge, consisting of edges and shifts.
Seek:
These problems need different feedbacks. Recurring coating worries removal completeness; excessive size worries dimensional consistency; scrapes issue glass problem.
Getting rid of the coating is not the last step. Abrasive particles, glass fines, taking care of residues, and improper cleaner can jeopardize the processed surface area.
Make use of an approved cleaning treatment compatible with the glass, coating, and sealer system. Secure refined panes from contamination before setting up and specify any kind of needed limitations on storage or handling.
A visually tidy surface area does not instantly show that the bonding interface is suitable.
Acceptance standards need to be specific enough that experienced examiners can get to constant choices. Most importantly, distinguish the coating manufacturer’s demands from interior factory targets.
A maker might embrace a narrower operating variety to reduce procedure variation, yet that range has to be sustained by the approved item spec and engineering proof.
| Characteristic | Approval need | Typical failing |
|---|---|---|
| Elimination completeness | Called for finish layers eliminated from the specified zone | Recurring covering |
| Removal size | Within documented dimensional limitations | Band as well slim or too broad |
| Perimeter connection | Needed removal is continuous | Unrefined areas or edges |
| 유리 상태 | Meets relevant surface and edge-damage standards | Scratches or chips |
| Cleanliness | Fulfills accepted preparation requirements | Abrasive residue or contamination |
| Pane alignment | Matches the defined setup | Incorrect surface area refined |
| Tools problem | Configuration and consumables fulfill accepted demands | Worn tooling or unstable monitoring |
| 추적 가능성 | Called for inspection documents are total | Missing out on dimensions or launch evidence |
First, define the measurement reference. Assessors need to know where the measurement starts and ends; otherwise, apparently exact analyses might not be equivalent.
The control strategy must define the dimension tool, evaluation locations, nominal target where suitable, minimum and maximum limits, and treatment of corners.
Dimensions ought to cover depictive positions along the called for edges, with added checks where the procedure is recognized to differ.
Do not develop an universal millimetre tolerance. The appropriate width depends upon the covering, sealer plan, spacer geometry, and producer requirements. Where the authorized spec specifies just a minimum or otherwise specifies the geometry, any kind of additional limit needs technical validation.
The best control system recognizes variation before it develops nonconforming glass. Last evaluation continues to be needed, yet it should not be the only guard.
| 이슈 | Possible reason | Suggested action |
|---|---|---|
| Residual layer | Worn unpleasant or irregular call | Confirm tooling and removal efficiency |
| Extreme width | Incorrect positioning or program | Procedure all edges and confirm placement |
| Uneven band | Tracking or feed variation | Check mechanical repeatability |
| Scrapes or chips | Abrasion or managing damage | Hold the pane for evaluation |
| Contamination | Inadequate cleaning or taking care of | Apply accepted cleaning and reinspect |
| Corner issues | Incomplete course shifts | Confirm corner settings |
| Issues after upkeep | Configuration not restored correctly | Repeat configuration confirmation and first-piece authorization |
When a defect appears, include possibly affected glass before spacer positioning and sealing. Identify the last known appropriate assessment factor, figure out the afflicted manufacturing interval, and record the disposition of each nonconforming pane.
Remodel ought to be licensed for the specific product. A 2nd elimination pass may get rid of residual covering however can additionally expand the band or introduce damages. If conformity can not be demonstrated, decline the pane as opposed to repeatedly grinding it in an effort to boost look.
Requirements need to be used within their actual range. An architectural glass requirement does not immediately define coating-removal resistances.
Together, these referrals strengthen the need to separate structural efficiency, sealer compatibility, and manufacture acceptance. Each requires appropriate evidence.
A valuable control strategy translates technological needs into repeatable production decisions.
| Control | Required documentation |
|---|---|
| Item recognition | Glass type, covering reference, measurements |
| Refine setup | Device program, operating specifications, unpleasant condition |
| First-piece authorization | Inspection results and gauged size |
| In-process checks | Sampling frequency, locations, recorded results |
| 유지 관리 | Tool adjustments, calibration, setup confirmation |
| Nonconformance | Issue type, control, approved personality |
| Final release | Examination condition and traceability records |
First-piece approval is especially vital after upkeep, finish adjustments, or devices adjustments. Periodic examination ought to after that reflect procedure security, historical defects, and the risks connected with the product.
Where adequate reliable dimensions exist, statistical process control can aid recognize patterns before the process goes across a spec limitation. Inner activity limitations need to cause examination before product acceptance limits are breached.
The goal is not a lot more paperwork. It is previously detection and fewer malfunctioning panes reaching assembly.
Edge deletion must be collaborated with the actual glazing item and its downstream requirements.
For 맞춤형 크기의 웜엣지 에너지 절약 유리, confirm that the deletion geometry works with the specified spacer and sealant plan.
Jobs entailing laminating-ready bent toughened up glass might present extra geometry and managing restrictions. Flat-glass assumptions need to not be moved without technical testimonial.
Similarly, blast-mitigation glass with enhanced retention has performance requirements expanding beyond side preparation. Passing a removal inspection does not develop that the full glazing system satisfies its safety and security goals.
Each product requires a specification suitable to its building and construction and intended application.
Low-E side deletion is the regulated removal of defined low-emissivity finishing from designated glass edges prior to shielding glass assembly. It develops the needed side condition for the authorized sealing system and can reduce coating-related durability risks. The precise elimination geometry and acceptance needs depend on the finishing product and IGU arrangement.
Side removal is called for when the coating manufacturer or accepted IGU setup defines covering elimination in the edge-seal area. For relevant soft-coat items, this helps establish the desired sealant-to-glass user interface and lower possible deterioration or delamination. Demands differ by product, so suppliers should comply with the suitable technical documents.
The acceptable Low-E edge deletion width is the dimensional array defined for the coating, spacer plan, sealant system, and task. No single width should be thought to use globally. The manufacturing spec should define dimension recommendations, applicable tolerances, and examination techniques utilizing accepted technological demands.
Manufacturers examine coating elimination efficiency by checking the designated side zone with a technique suitable for the finishing and acceptance requirements. Visual evaluation can determine obvious residue and interruptions, while dimensional tools action removal width. Extra verification might be essential when visual evaluation can not accurately find remaining coating layers.
Low-E edge deletion issues occur from tools wear, incorrect setup, irregular glass positioning, contamination, managing damage, or inadequate evaluation. Typical failings include recurring finish, excessive removal size, irregular removal, and scratches. Root-cause evaluation should compare the problem pattern with equipment setups, unpleasant problem, production documents, and product demands.
Incorrectly removed Low-E glass can be revamped just when the authorized item requirements allow the proposed adjustment without jeopardizing glass problem or the securing interface. Added grinding might get rid of residual finishing yet can likewise widen the band or damage the surface area. Remodel should be licensed, evaluated, and recorded.
ASTM E1300 deals with the tons resistance of glass in structures as opposed to universal coating-removal tolerances. It supports architectural glass style yet must not be dealt with as the single authority for removal size or coating-removal efficiency. Those requirements need to originate from suitable item documents and the approved job requirements.
Producers can lower edge removal prices by enhancing process security, preventing repeat issues, enhancing abrasive life, and recognizing nonconforming glass prior to assembly. Helpful indicators consist of first-pass return, defect frequency, rework hours, and price per approved pane. Throughput improvements have to remain within approved technological needs.
A pane should be released just when it satisfies the suitable demands for layer elimination, removal geometry, glass problem, cleanliness, and traceability.
The greatest production procedure defines the spec, manages the equipment, gauges the completed side, and contains problems before setting up. It then utilizes taped production data to enhance consistency.
A clean-looking side is a useful observation. It is not proof of consistency.
Required a more trusted glass manufacture requirements? Confirm your layer maker’s needs, coordinate edge deletion with the designated IGU sealing system, and develop evaluation requirements your production and quality teams can use continually. Discover custom-size energy-saving glass solutions when aligning product requirements with job needs.